In biopharmaceutical manufacturing, single-use systems have become an integral part of processes ranging from R&D to commercial production, thanks to their flexibility, reduced risk of cross-contamination, and reduced cleaning and validation burden. The quality of single-use consumables can directly affect drug safety and efficacy.
Evolution of Single-use Consumables
Late 1970s
The biopharmaceutical industry began experimenting with simple plastic containers as alternatives to traditional glassware, marking the early development of single-use consumables. At the time, these were mainly plastic bags used in small-scale R&D applications.
1990s
With the introduction of rocking single-use bioreactors, single-use systems with capacities ranging from 50 L to 1,000 L began to be adopted for industrial applications. However, high-performance single-use consumables and critical film materials remained largely supplied by international manufacturers, resulting in long procurement lead times and supply uncertainties for Chinese pharmaceutical companies.
After 2010
As monoclonal antibodies, vaccines, and cell therapies expanded rapidly, the industry increasingly recognized the limitations of traditional stainless-steel production lines, including costly retrofits, extensive cleaning validation requirements, and limited flexibility for product changeovers. With their lower contamination risk, faster deployment, and greater flexibility for multi-product manufacturing, single-use consumables gradually became a mainstream choice. Over the past decade, the localization of China’s biomanufacturing supply chain has accelerated, with domestic consumables manufacturers emerging across the country and gradually developing integrated capabilities spanning film selection, automated manufacturing, and comprehensive compliance testing and validation.
Morimatsu’s Single-use Consumables Manufacturing Capabilities
Morimatsu’s single-use consumables manufacturing base has established comprehensive in-house testing capabilities covering physicochemical testing, microbiological testing, sterility testing, and positive control testing.
Equipped with precision testing instruments, the facility performs in-house incoming inspection of raw and auxiliary materials as well as comprehensive finished-product release testing.
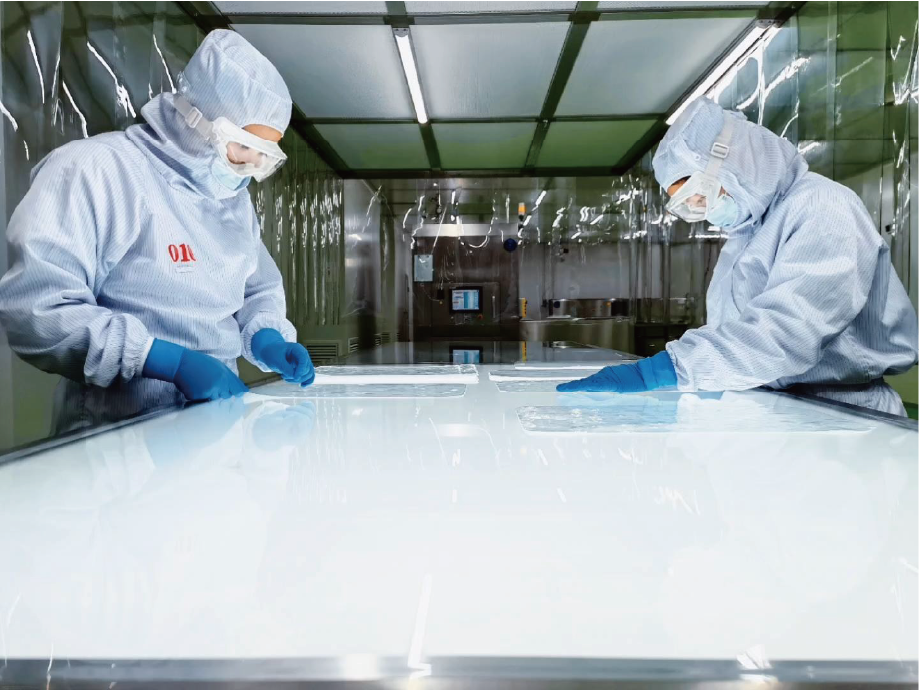
The site also features a 1,000 m² cleanroom production area incorporating Grade C and Grade A zones, together with a dedicated production line for biopharmaceutical single-use consumables.
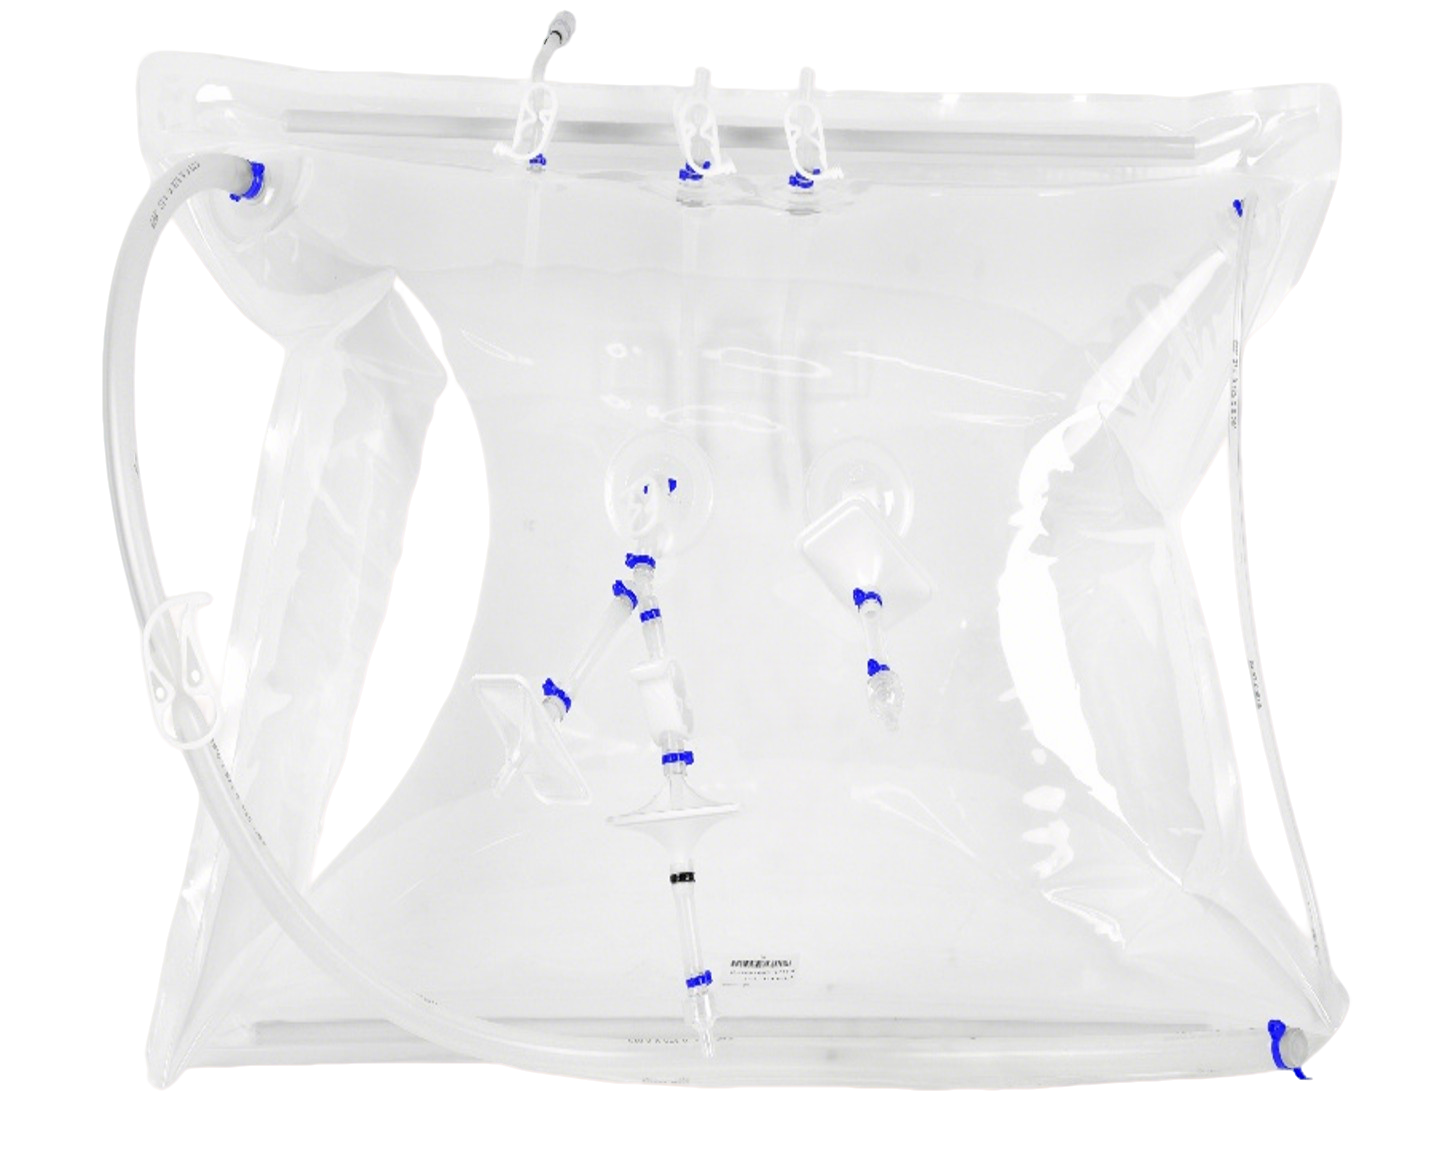
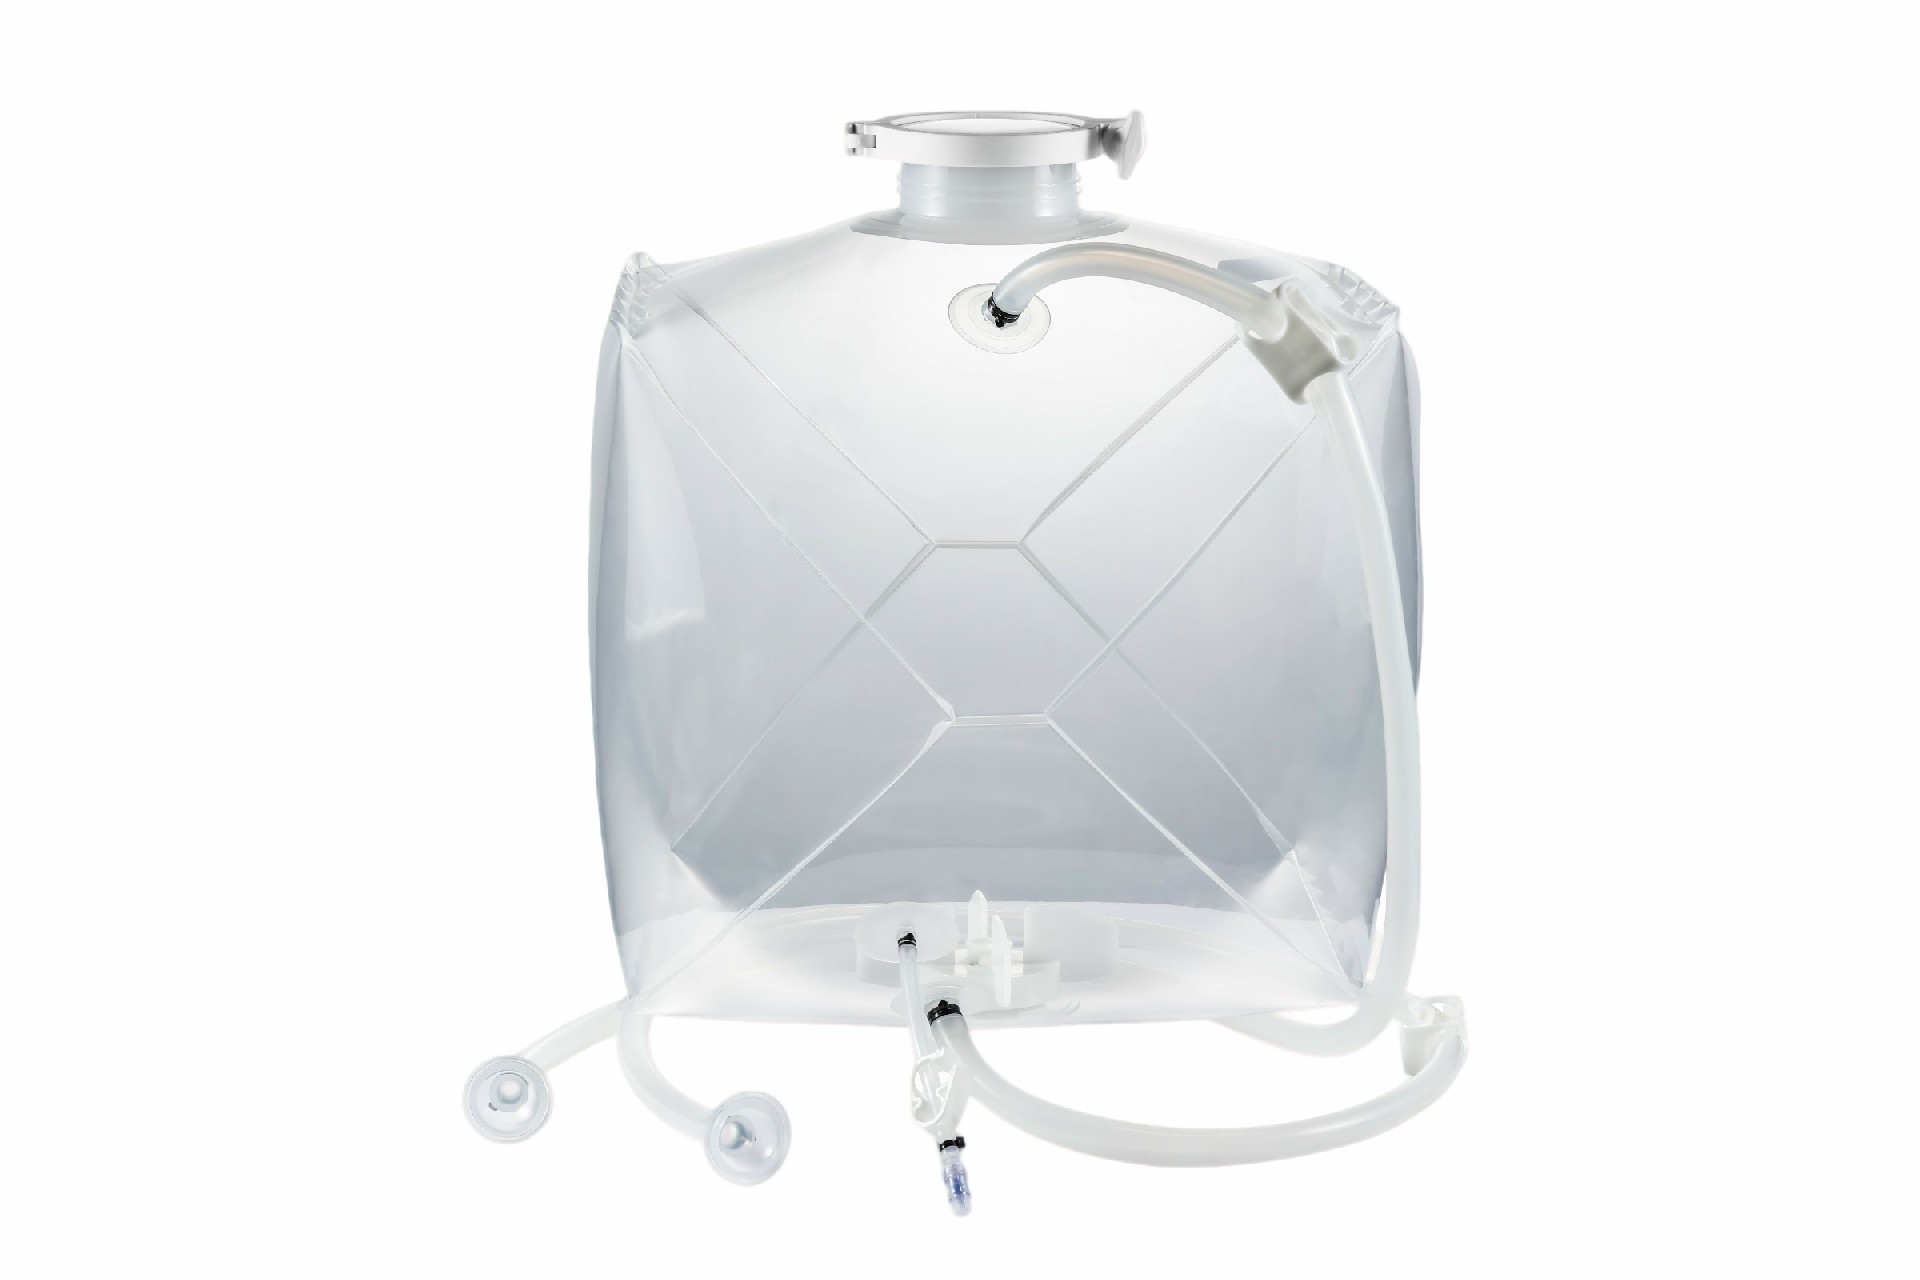
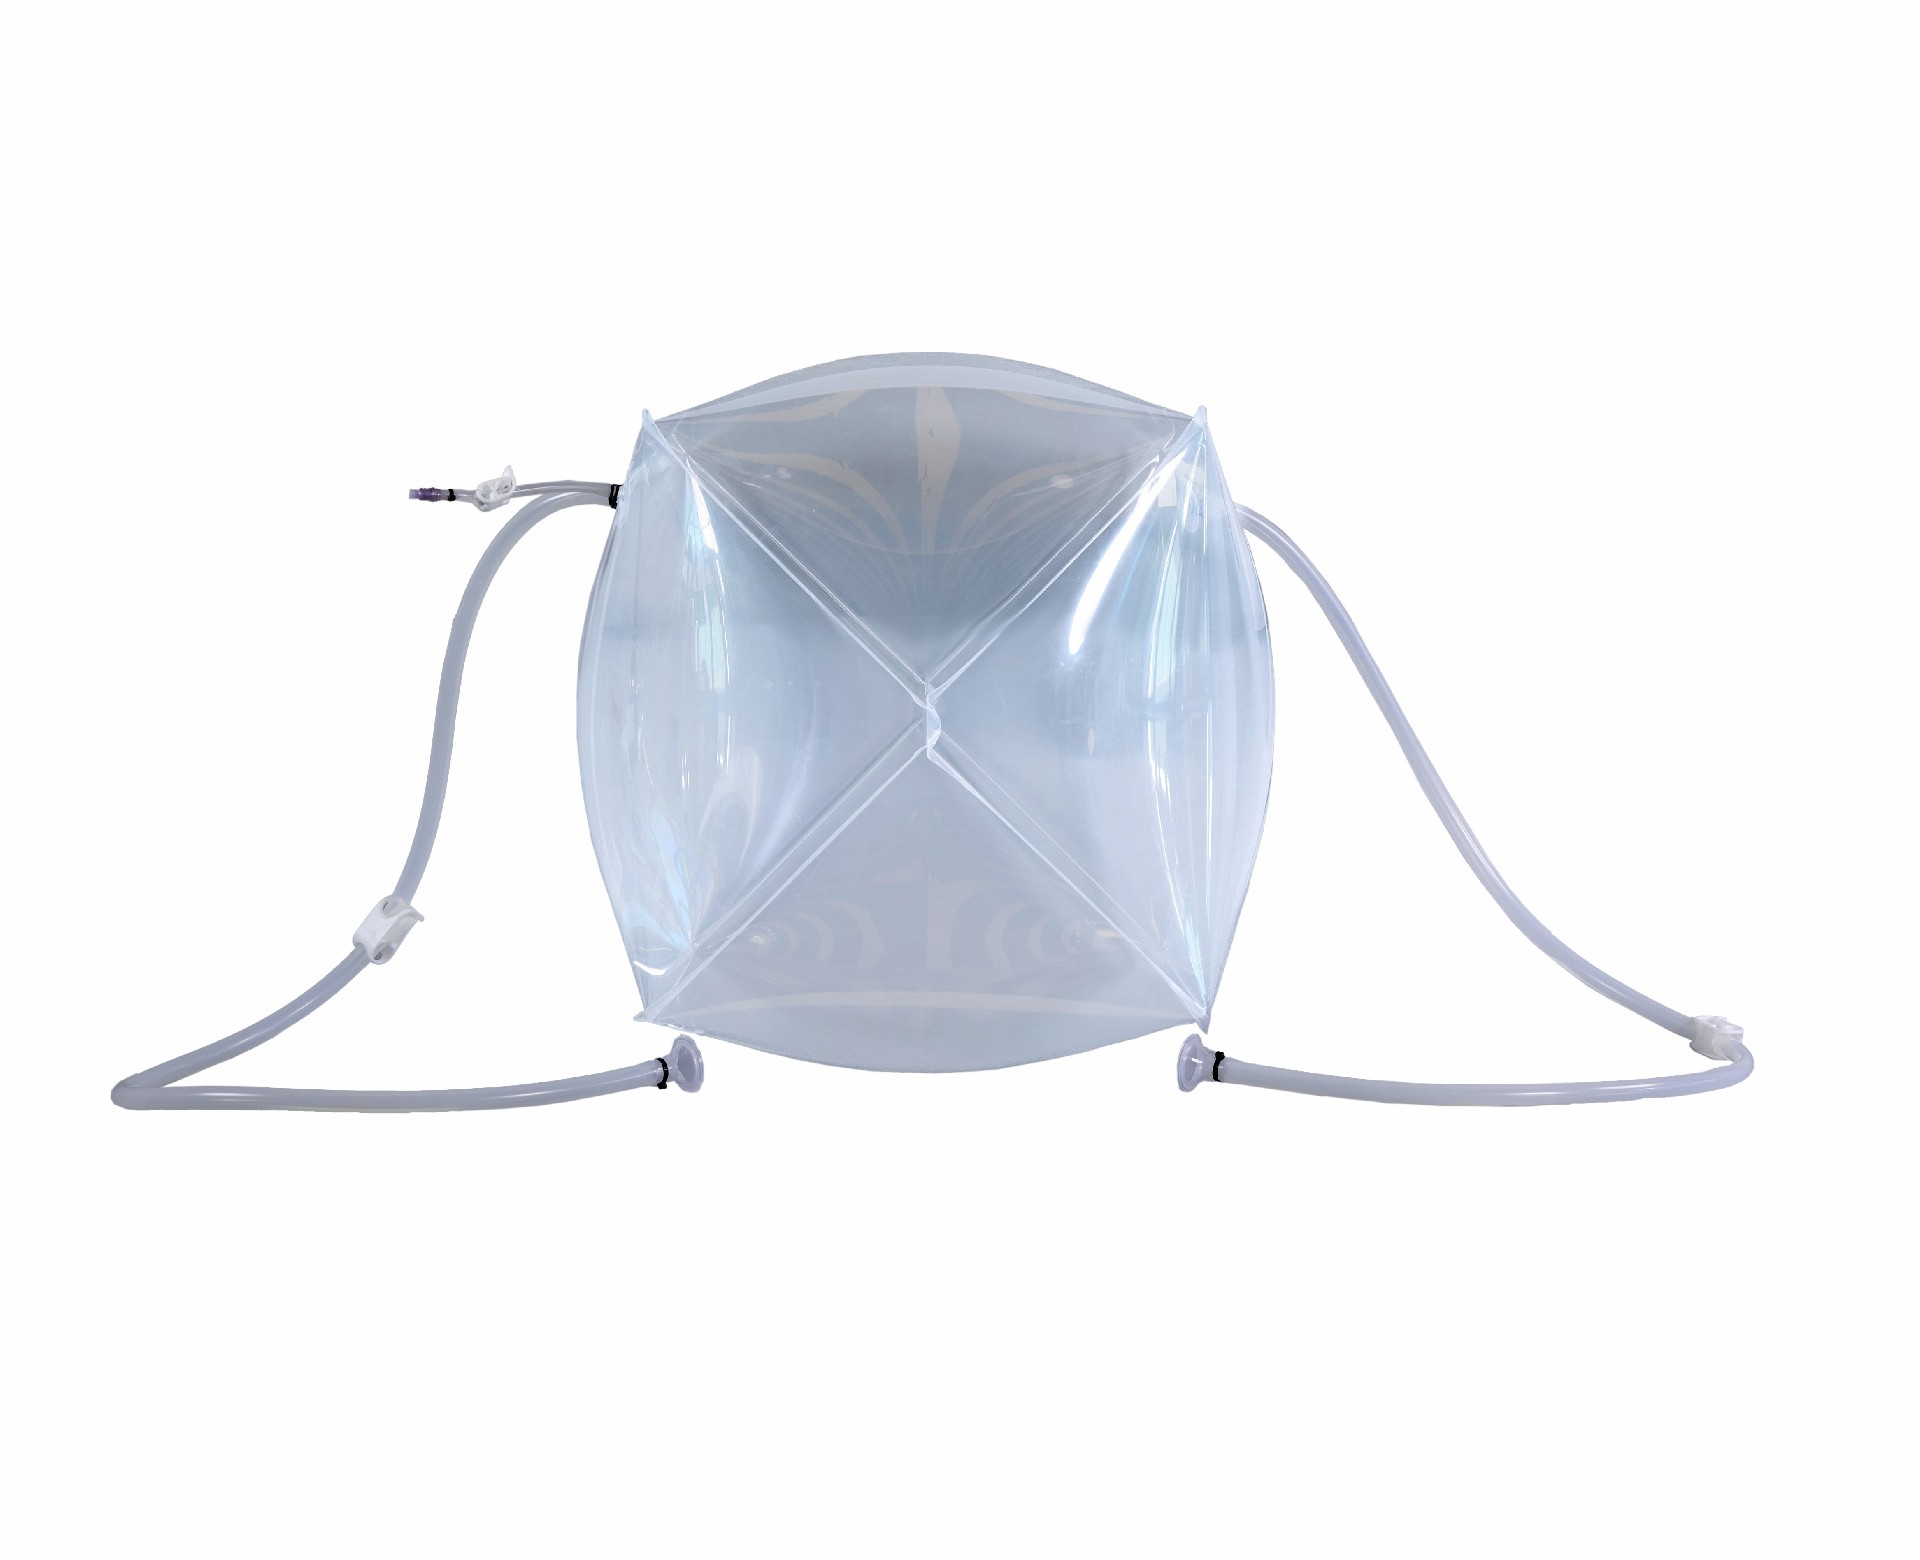
· Single-use Cell Culture Bags · Single-use Mixing Bags · Single-use Liquid Storage Bags
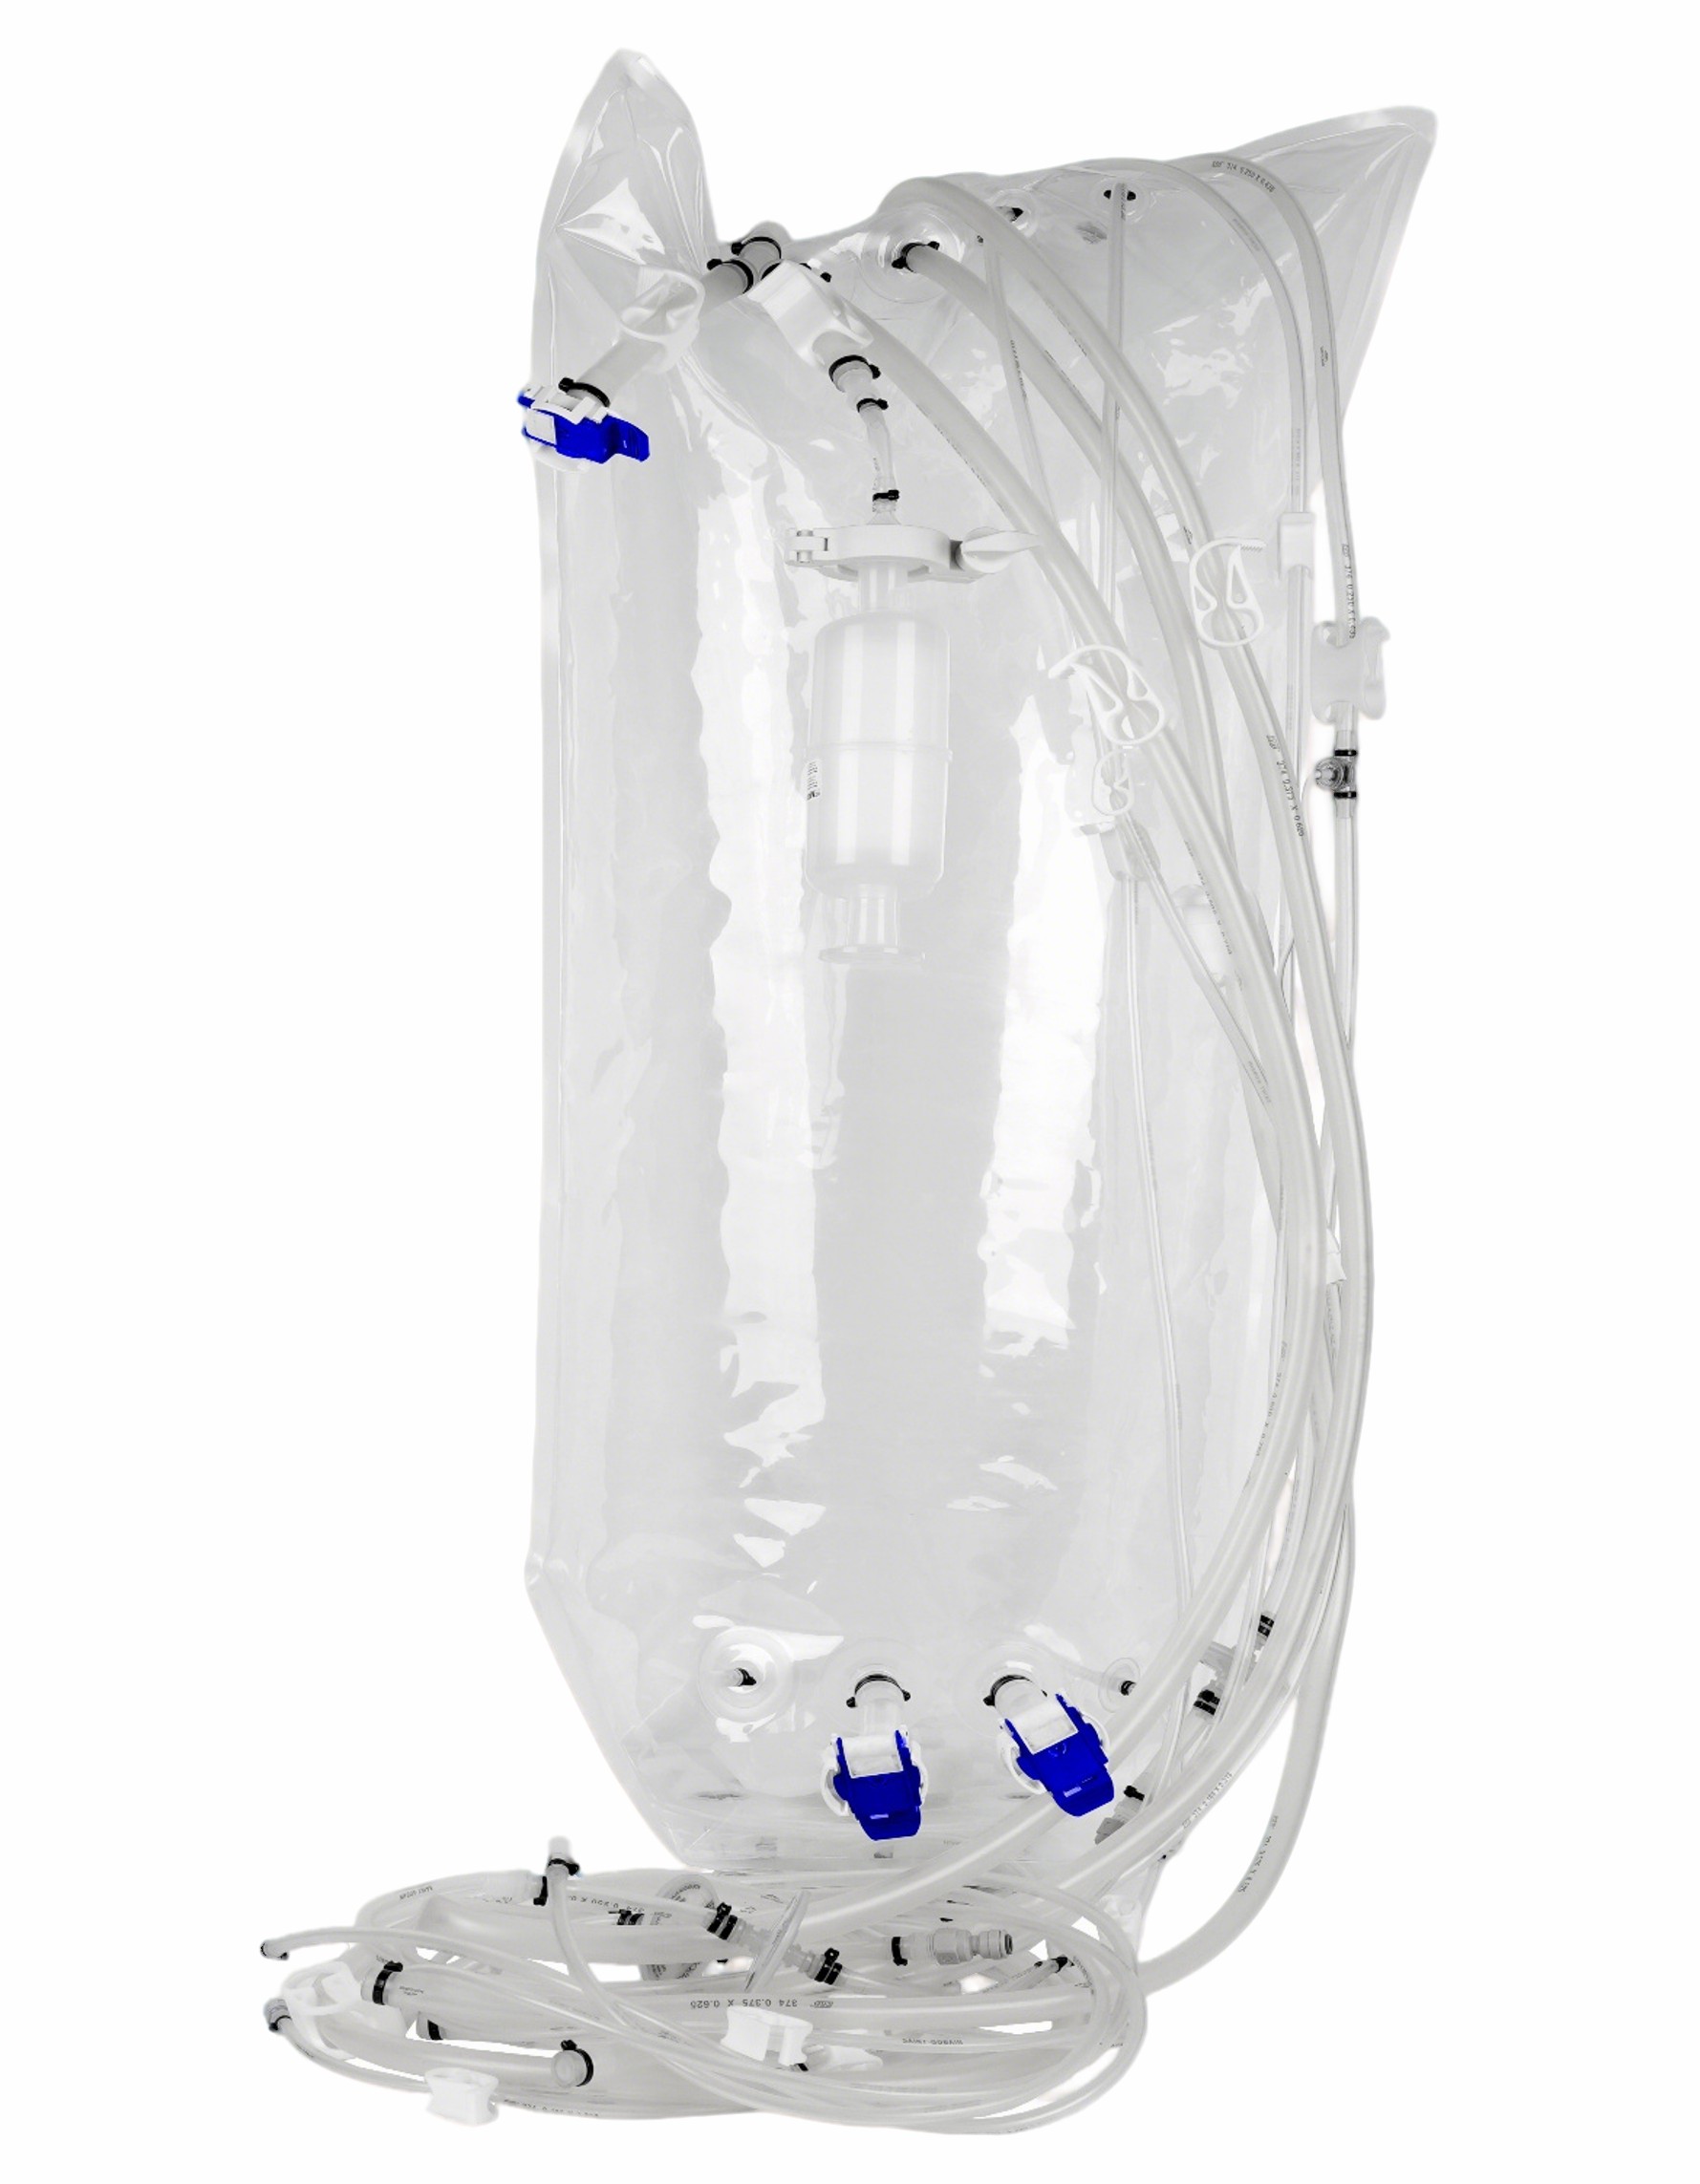
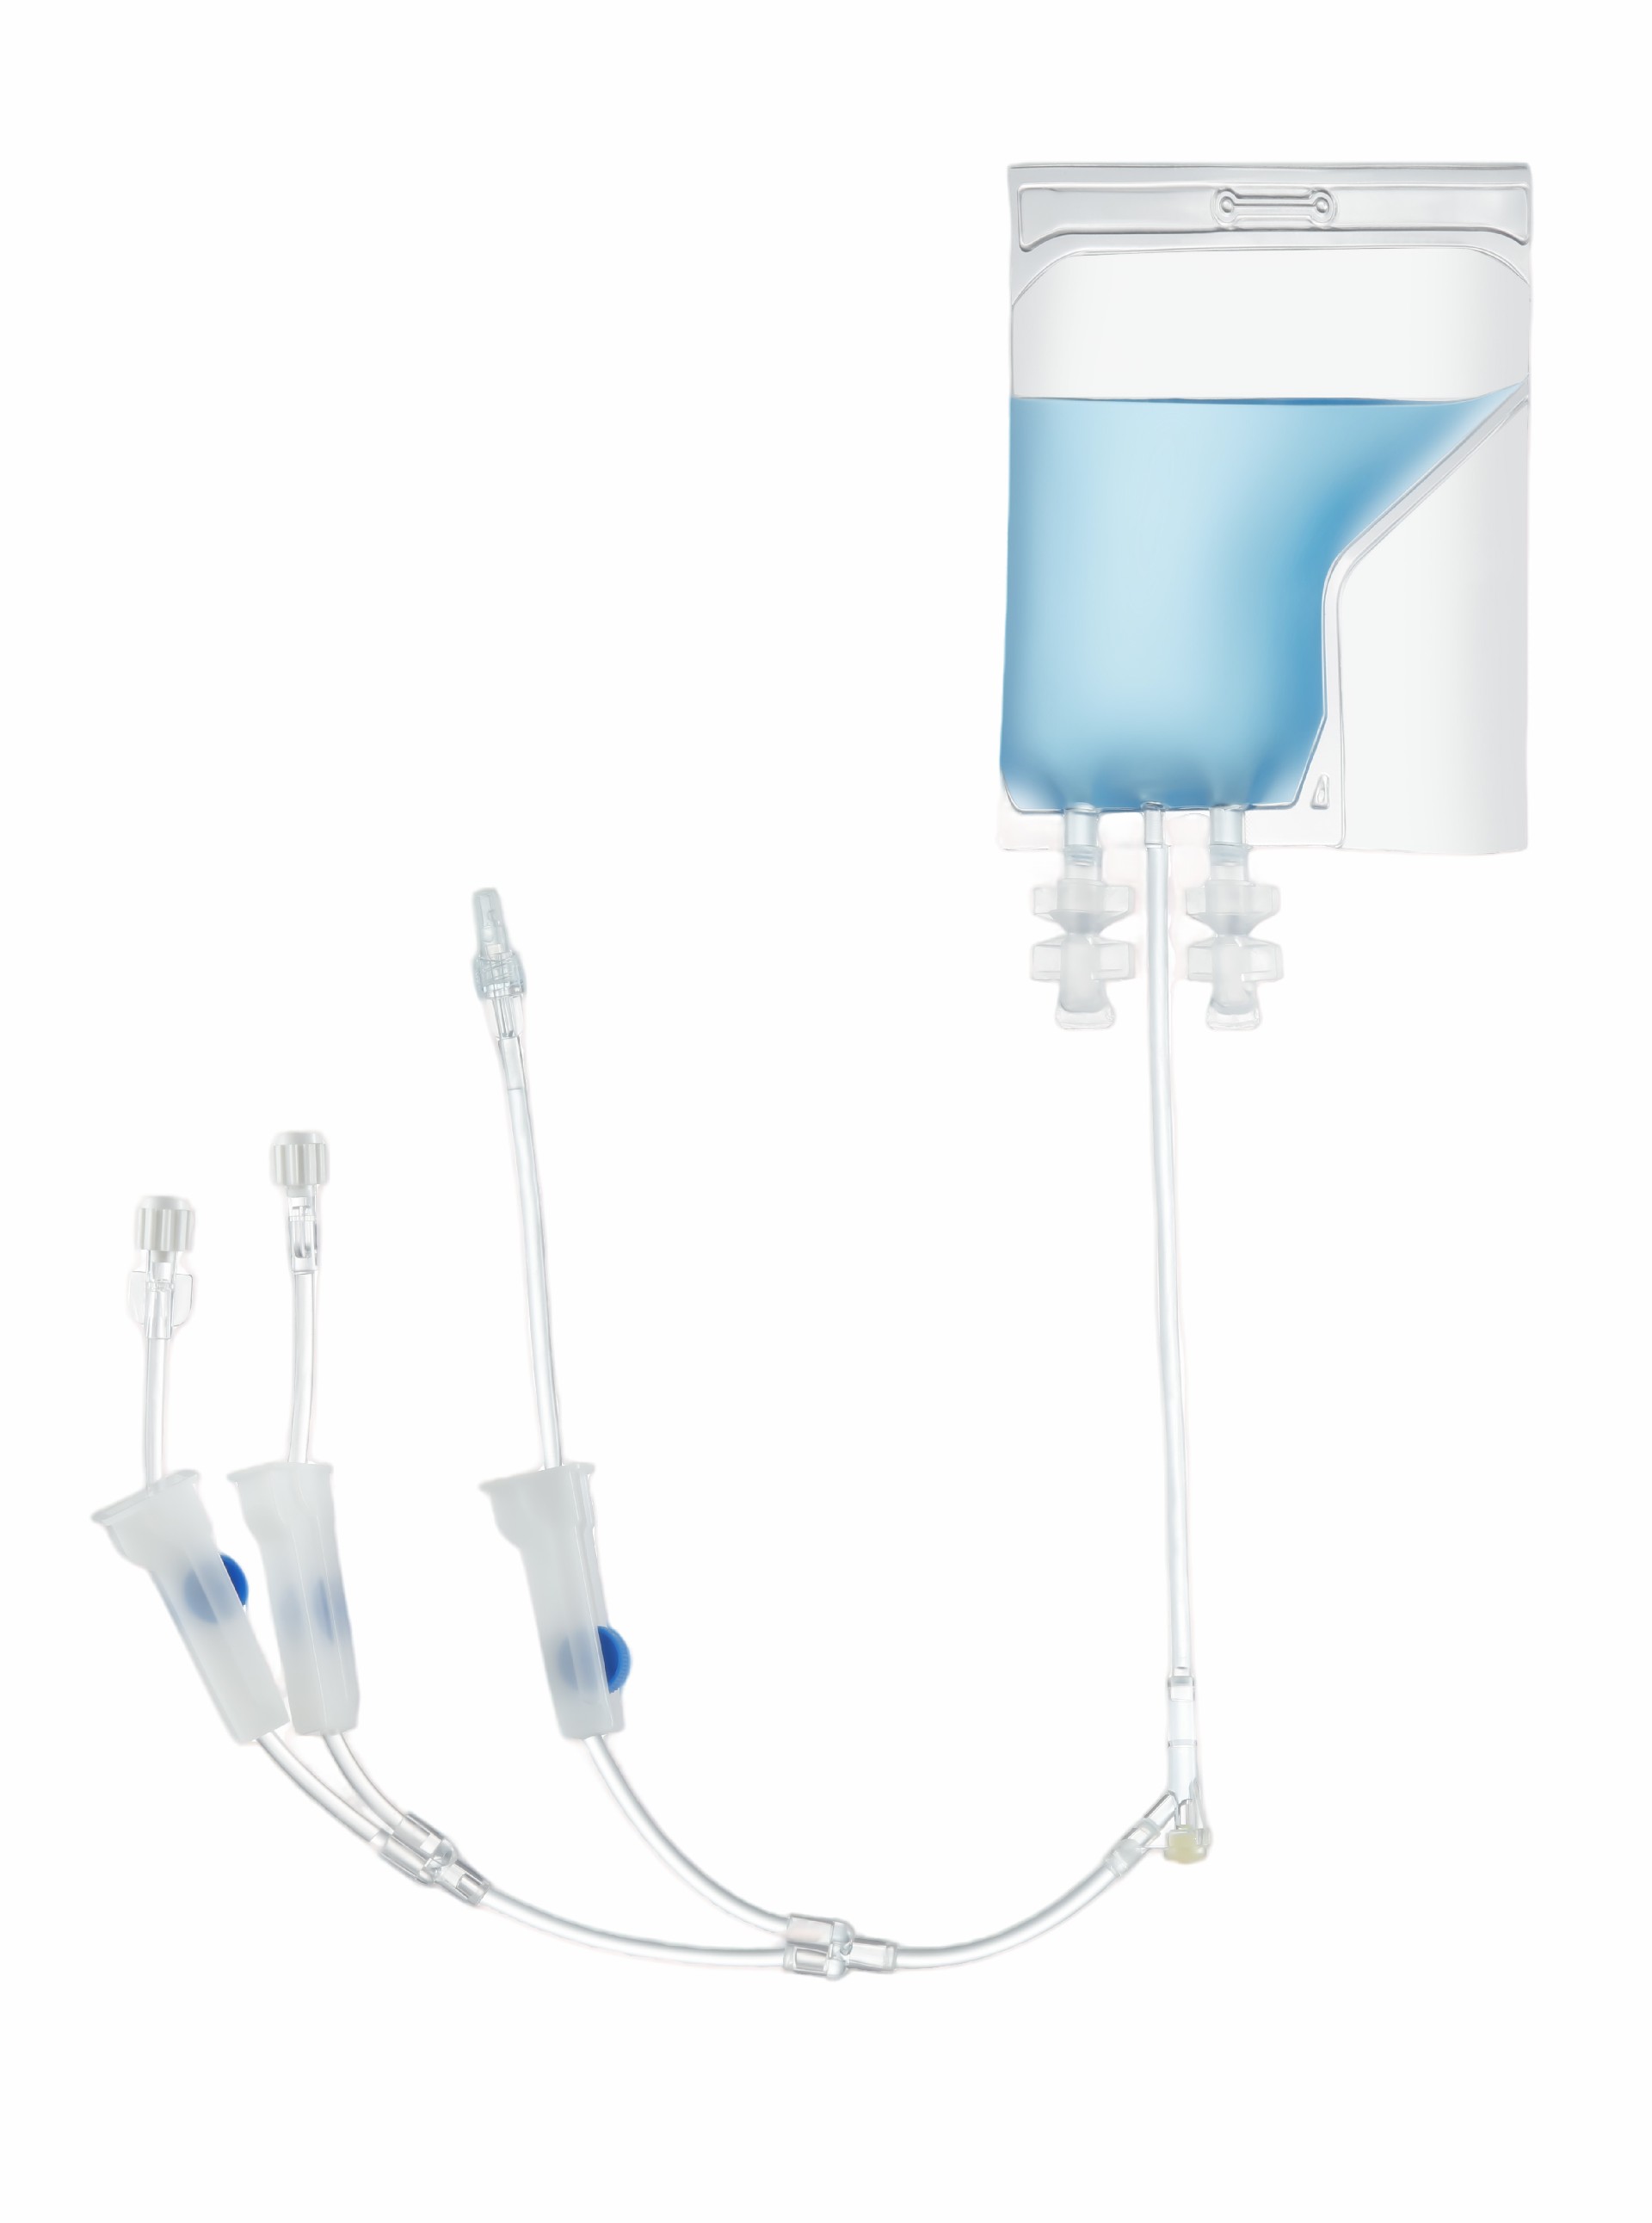
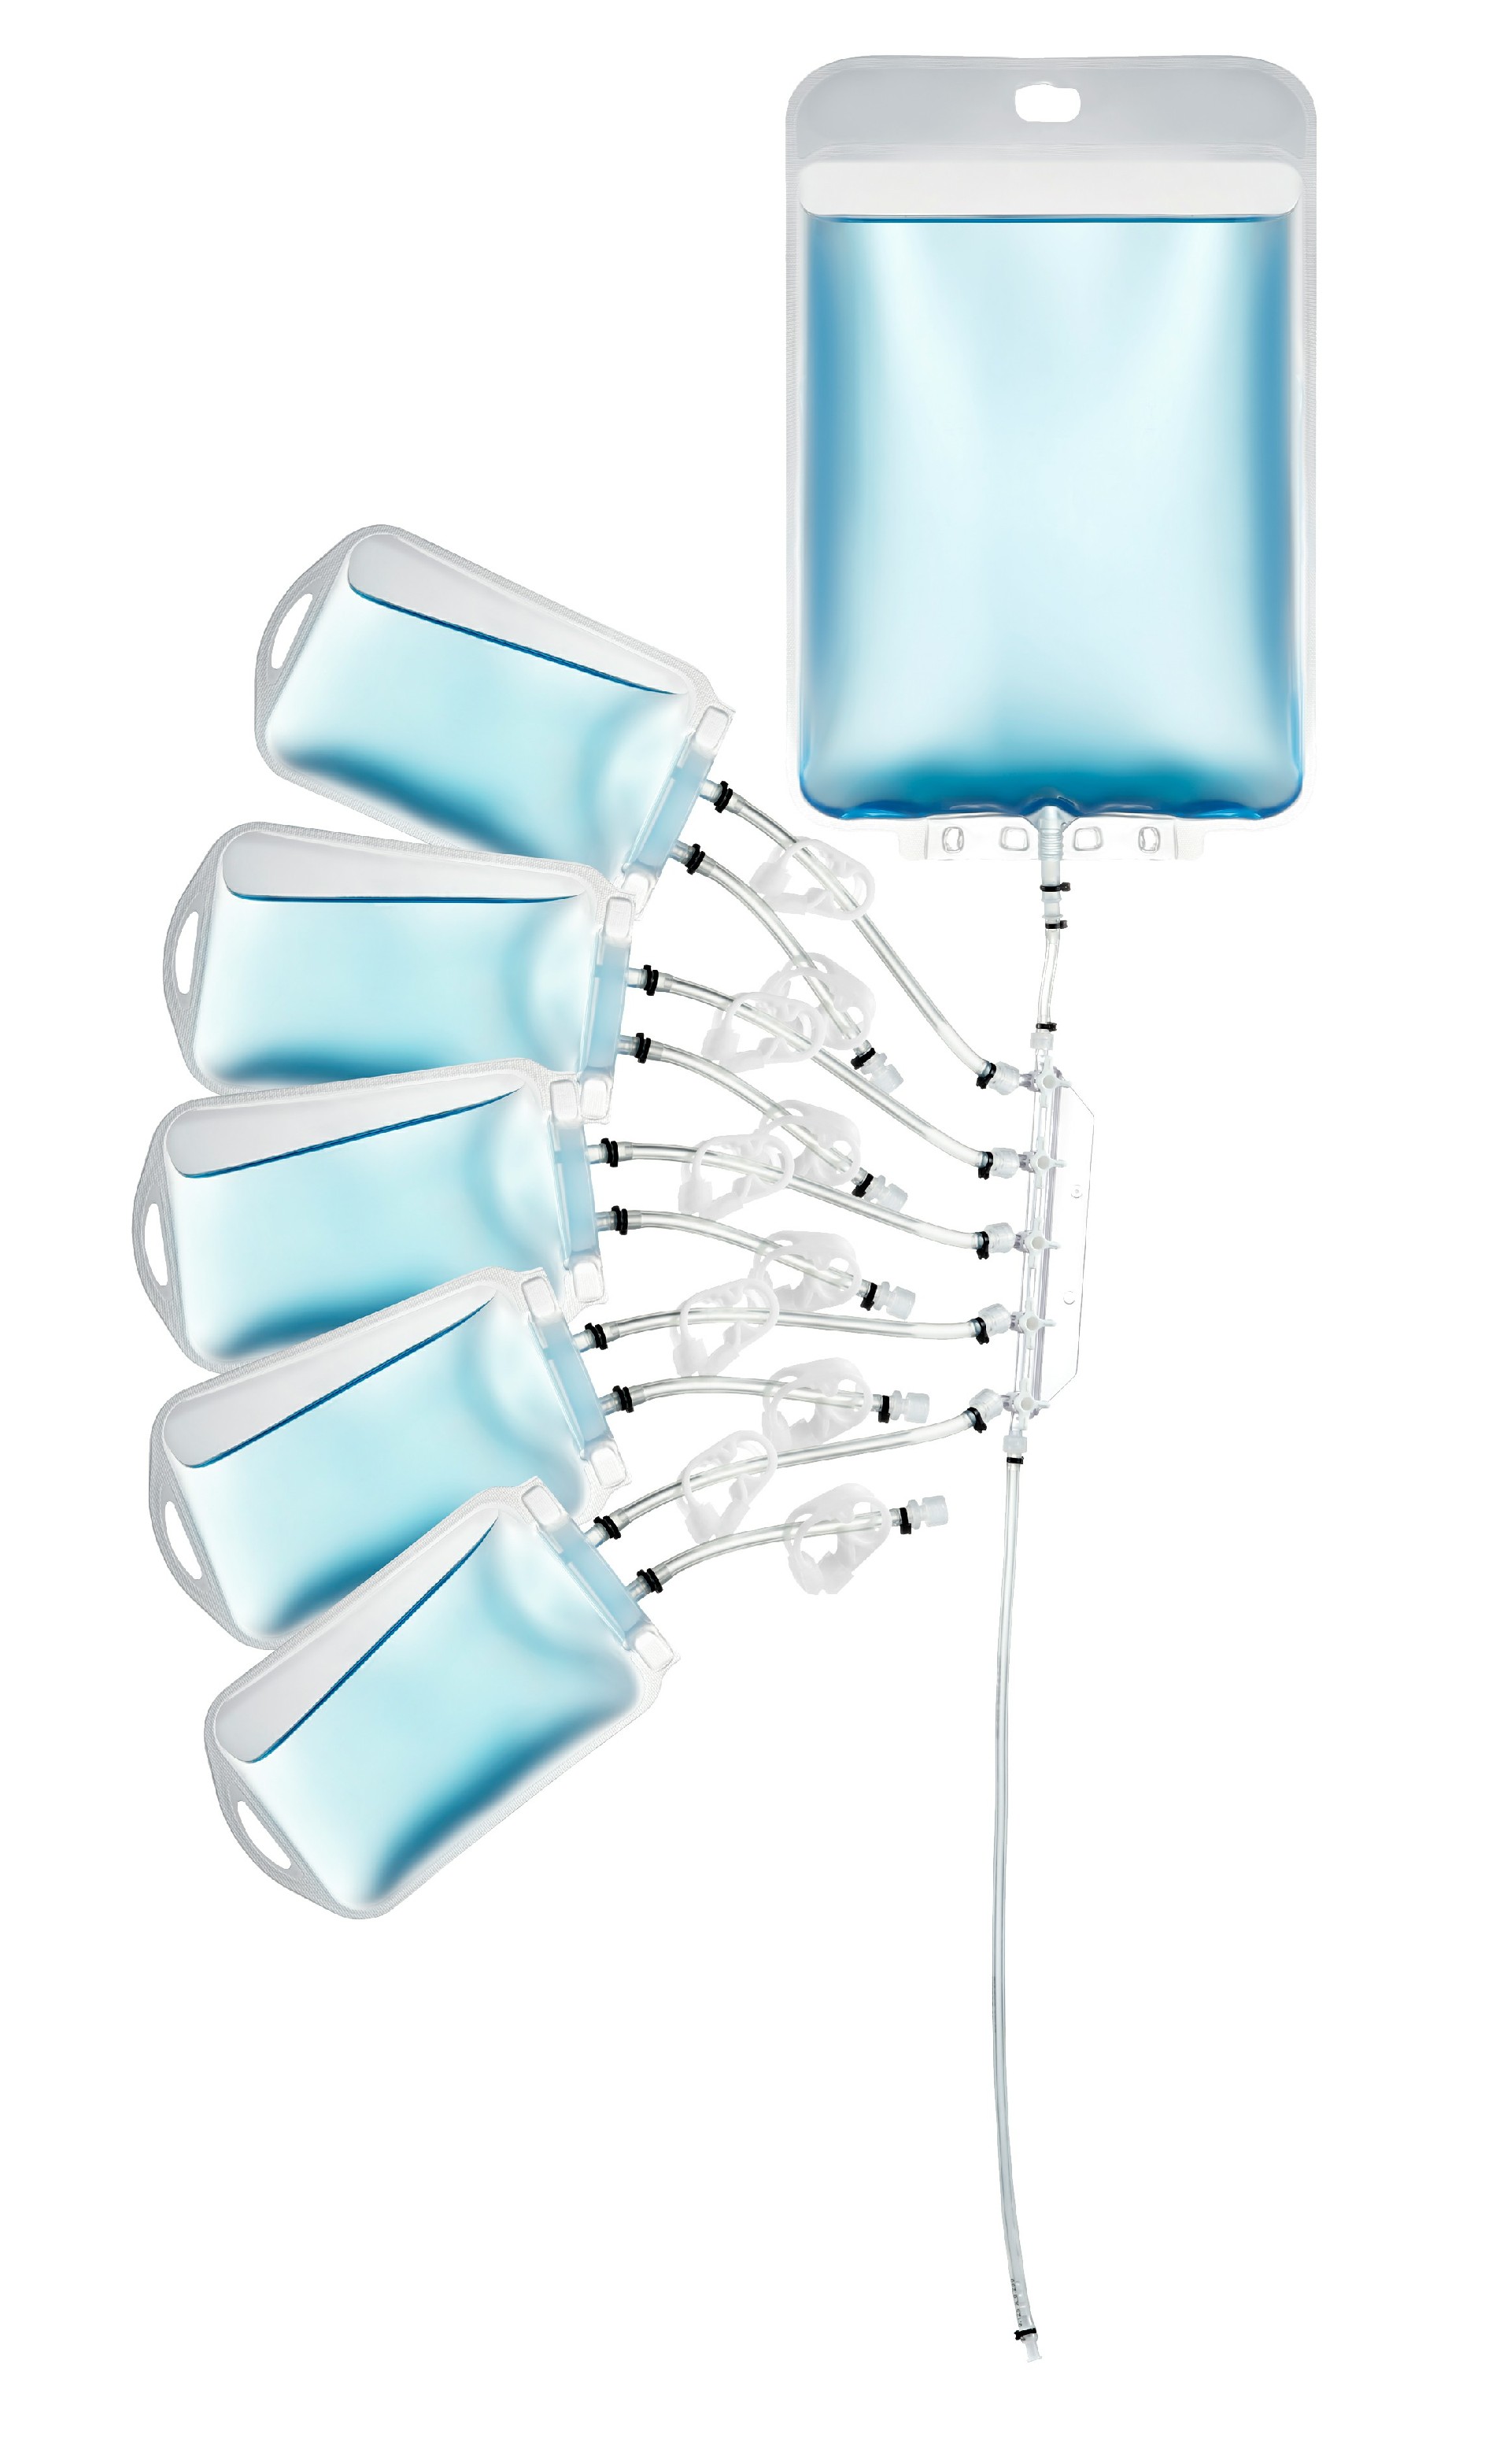
· Single-use Bioreactor Bags · Freezing Bags · Single-use Sampling Bags
Morimatsu also provides single-use tubing assemblies and other single-use components, including ports, tubing, filters, connectors, and accessories, with customized configurations available to meet specific customer requirements.
1. Rigorous Control from the Source:Carefully Selected Films for a Stronger Foundation of Safety
The performance of raw materials directly affects the levels of extractables and leachables, biosafety, and overall performance of single-use consumables.
Morimatsu’s single-use aseptic bags use imported medical-grade biopharmaceutical film with a multilayer structure comprising LDPE (low-density polyethylene), Tie, EVOH (ethylene-vinyl alcohol copolymer), Tie, and ULDPE (ultra-low-density polyethylene).
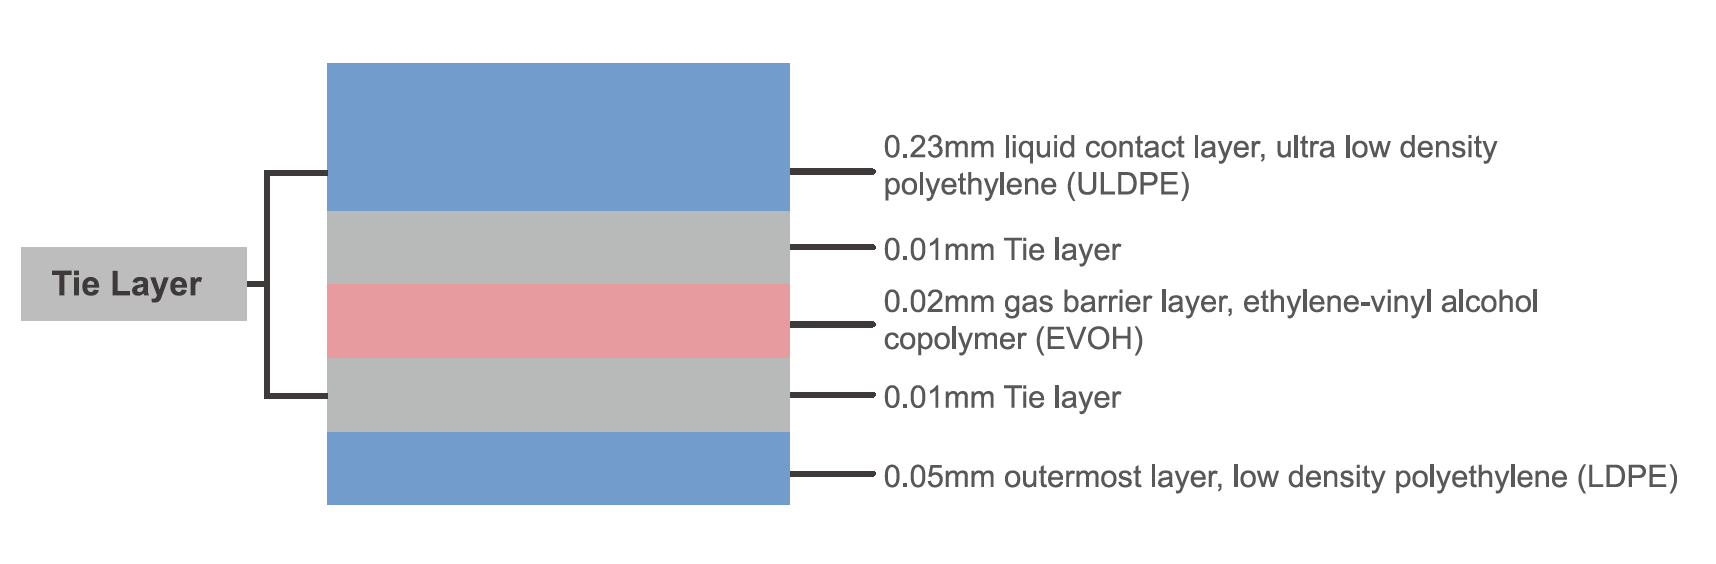
The film offers high mechanical strength, excellent puncture and tear resistance, good chemical inertness, and ultra-low levels of extractables and leachables. It contains no animal-derived components, helping mitigate TSE/BSE-related biosafety risks.
The material is well suited to demanding biopharmaceutical processes such as cell culture, protein purification, and formulation preparation, helping to minimize process risks from the outset.
2. Standardized Production:Standardized Processes with End-to-End Traceability
01 Environmental Control
After raw materials enter the production area, the main process steps are performed in a Grade C cleanroom environment, while critical operations such as welding are carried out under Grade A conditions. Workshop air is treated through primary, intermediate, and high-efficiency filtration systems, with a controlled air-change rate appropriate to the cleanroom classification. Temperature and humidity are continuously monitored and controlled, while equipment and floors are disinfected every shift to further minimize contamination risks.
02 Automated Manufacturing
The production line integrates automated film cutting, edge sealing and welding, integrity testing, and vacuum packaging, enabling core production processes to be completed within an integrated workflow. Operators perform self-inspections and cross-checks throughout production. Each semi-finished product is inspected, allowing potential production defects to be identified and addressed promptly.
03 Packaging and Sterilization
Qualified products are individually double-bagged in a clean environment and labeled with the batch number, expiration date, and sterilization code to ensure full product traceability. Following gamma irradiation and successful inspection, the products are transferred to a dedicated finished-goods warehouse.
04 In-Process Quality Control
Complete records are maintained throughout the entire production process, from incoming raw materials through to finished-product warehousing. This enables full traceability of material sources and destinations while ensuring strict adherence to applicable industry quality standards.
3. Quality System Assurance:Multi-Dimensional Controls Aligned with Pharmaceutical Audit Requirements
Morimatsu has established a comprehensive quality management system aligned with GB/T 19001-2016/ISO 9001:2015, GB/T 42061-2022/ISO 13485:2016, and ISO 15378:2017.
Supported by end-to-end on-site controls, the system establishes a multi-layered quality framework covering five key dimensions:
Continuous dynamic monitoring of the cleanroom environment
Periodic maintenance and qualification of production equipment
Tiered management and release of raw and auxiliary materials
Real-time monitoring of critical process parameters
Standardized management of technical documentation and production records
By standardizing operations throughout the manufacturing process, the system ensures end-to-end traceability and auditability while supporting the audit and compliance requirements of biopharmaceutical companies.
4. Comprehensive Validation:Comprehensive Testing to Support Process Quality and Compliance
A comprehensive validation data package is essential for the compliant use of single-use consumables.
Morimatsu conducts systematic product testing covering seal integrity, heat-seal strength, insoluble particulate matter, freeze-thaw performance, bacterial endotoxins, heavy metals, stability, and irradiation dose verification.
The resulting validation data support the safe and compliant use of single-use consumables across a wide range of biopharmaceutical applications, including upstream cell culture, downstream purification, and formulation and transfer processes.
As demand for biopharmaceutical products continues to grow, Morimatsu remains focused on advancing its single-use consumables capabilities. By applying rigorous quality standards and leveraging localized, scalable manufacturing capacity, Morimatsu helps ensure reliable product supply and delivery.
Through integrated, high-quality single-use consumables solutions, Morimatsu supports biopharmaceutical manufacturers in building more secure, efficient, and resilient supply chains.
About Morimatsu LifeSciences
Morimatsu LifeSciences is a key business segment of Morimatsu International Holdings Limited (Stock Code: 2155.HK). It comprises Shanghai Morimatsu Pharmaceutical Equipment Engineering Co., Ltd., Morimatsu (Suzhou) LifeSciences Co., Ltd., Shanghai Morimatsu Biotechnology Co., Ltd., Shanghai Mori-Biounion Technology Co., Ltd., Shanghai Morisora Technology Co., Ltd., Bioengineering AG, Pharmadule Morimatsu AB, and its affiliated companies.
Morimatsu LifeSciences is dedicated in providing core equipment, process systems, and smart modular facility solutions, and services for the pharmaceutical, biopharmaceutical, medical aesthetics, and fast-moving consumer goods (FMCG) sectors including (cosmetics, food, and health supplements), as well as data centers.
Our team comprises highly experienced professionals with deep expertise in process R&D, engineering design, advanced manufacturing, compliance and validation consulting, production execution, and intelligent operations. With broad experience across diverse industries, we fully understand the unique characteristics and process requirements of various products. This enables us to deliver tailored, end-to-end process solutions from the conceptual design stage, precisely aligned with client’s specific needs.
Morimatsu LifeSciences has established a strong global presence, supported by advanced R&D centers, design hubs, and state-of-the-art manufacturing facilities worldwide. Our well-established service network spans Europe,USA,Asia-Pacific, and emerging markets. We have successfully delivered outstanding, customized solutions to clients in over 40 countries and regions, gaining extensive experience in international project execution.
As a multinational enterprise with core strengths in process technology, modular facility construction, and intelligent manufacturing, Morimatsu LifeSciences is dedicated to meeting the evolving equipment and system needs of our key industries. Through continuous innovation and technological advancement, we are steadily expanding our global footprint, driving our international strategy forward, and delivering Morimatsu’s expertise, reliability, and innovation to the global life sciences and related sectors.